


Checkweigher for Mugwort Granules
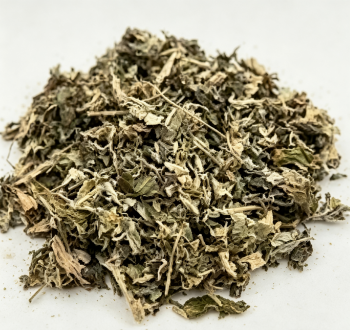
Customer Application
A manufacturer of traditional herbal medicine products needed to inspect the weight of bagged mugowrt granules on its production line. The client wanted a solution that could inspect product weight without interrupting production, improbe inspection efficiency, and ensure that each bag met the specified weight requirements.
Because the upstream production line was elevated, stable product transfer was also an important consideration. The client needed a system that could prevent bags from falling or moving off the conveyor belt during conveying while minimizing the influence of airflow on weight accuracy.
Inspection Requirements
The bagged mugwort granules were conveyed from a higher upstream production line to the weighing section for continuous weight inspection. Due to the height difference between the upstream line and the weighing system, the bags could fall or move off the conveyor belt during conveying.
In addition, airflow from the surrounding production environment could affect the stability of the weighing process and potentially influence measurement accuracy.
Based on these conditions, the checkweigher needed to provide:
• Stable conveying of bagged mugwort granules from the upstream line
• Effective control of bag movement on the conveyor belt
• Reduced interference from surrounding airflow
• Continuous and accurate weight inspection without interrupting production
Checkweighing Solution
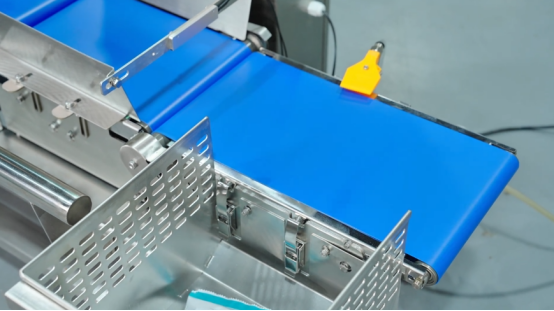
COSO provided a checkweigher solution configured specifically for the client's bagged mugwort granules and production line. The system includes a transition section and a weighing section. Adjustable baffles are installed on both sections to help keep the bags centered on the conveyor belt during conveying.
The baffles on the transition section help prevent the bags from moving off the conveyor when they enter the system from the higher upstream production line. The baffles on the weighing section further help maintain stable bag positioning during weighing. A wind shield is also installed around the weighing section to reduce the interference of airflow from the surrounding production environment. This helps create more controlled weighing conditions and supports stable weight inspection.
Testing Process
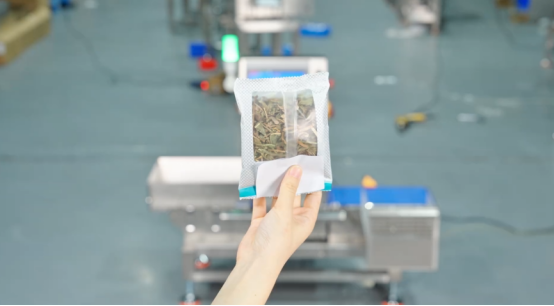
During the test, bagged mugwort granules were conveyed from the upstream production line into the checkweigher through the transition section. The adjustable baffles helped keep the bags properly positioned on the conveyor belt during conveying and reduced the risk of bags moving off the belt. The bags then entered the weighing section, where the wind shield helped minimize the interference of surrounding airflow.
The checkweigher continuously inspected the weight of each bag and compared the weighing value with the preset weight range. Bags outside the specified weight range could be automatically rejected according to the configured settings. An air-blast rejection system can be integrated, making the checkweigher suitable for high-speed lines with small packages. Products that are either underweight or overweight are automatically rejected from the production line.
Conclusion
For traditional herbal medicine production, consistent product weight is an important part of production control. When bagged products are conveyed from a higher production line, product movement and environmental airflow can affect the stability of the weighing process. For this bagged mugwort granule application, COSO designed adjustable baffles and a wind shield around the weighing section to address the client's specific production conditions.
The checkweighing solution provides continuous weight inspection while supporting stable product conveying and controlled weighing conditions, making it suitable for inline weight inspection of bagged mugwort granules in herbal medicine production.


